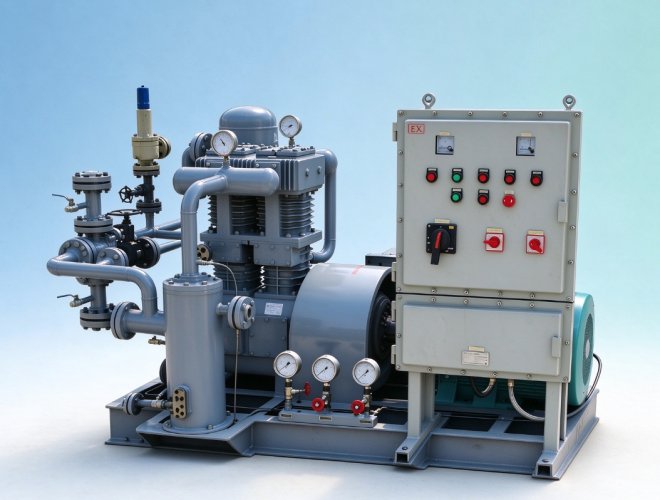
The BOG compressor is dedicated equipment for boil-off gas recovery from LNG storage tanks. Continuous low-temperature boil-off gas (BOG) is generated in LNG tanks due to heat ingress from the surroundings. The BOG compressor boosts the pressure of low-pressure, low-temperature BOG and delivers it to the recondenser for re-liquefaction, or back to fuel gas networks and export pipelines. It reduces natural gas venting loss, improves plant economy and maintains stable tank pressure.
Working Principle
Low-pressure BOG from the storage tank enters the compressor and is pressurised via multi-stage compression. Gas temperature rises during compression. An inlet knockout drum and cooler are fitted to prevent liquid carryover and unit damage. The pressurised BOG is fed to the recondenser to exchange heat with LNG for re-liquefaction, or supplied to the system as fuel gas. The unit is equipped with pressure interlocks to enable automatic start/stop and speed regulation based on tank pressure.
Core Advantages
✅ Suitable for wet low-temperature BOG service; inlet liquid separation protection against liquid slugging
✅ Optional types: reciprocating or centrifugal. Reciprocating for low flow rates, centrifugal for high flow rates
✅ Automatic pressure control with variable-frequency load adjustment responding to tank pressure
✅ Comprehensive interlock protection: shutdown triggered by abnormal oil pressure, temperature, vibration, liquid level and overpressure
✅ Skid-mounted assembly with inlet separator, cooler, safety relief valves and instrumentation
✅ Reduces BOG flaring, saves feed gas and meets environmental requirements
Technical Parameters (Example)
Medium: LNG boil-off gas (BOG, mainly methane)
Inlet Pressure: 0.005~0.08 MPa
Outlet Pressure: 0.6~1.6 MPa (customised for recondenser or fuel gas network)
Inlet Temperature: -130~-80 °C
Control Mode: DCS remote monitoring, automatic pressure regulation
Applications
BOG recovery systems for LNG liquefaction plants, LNG tank farms, LNG filling stations and LNG receiving terminals